
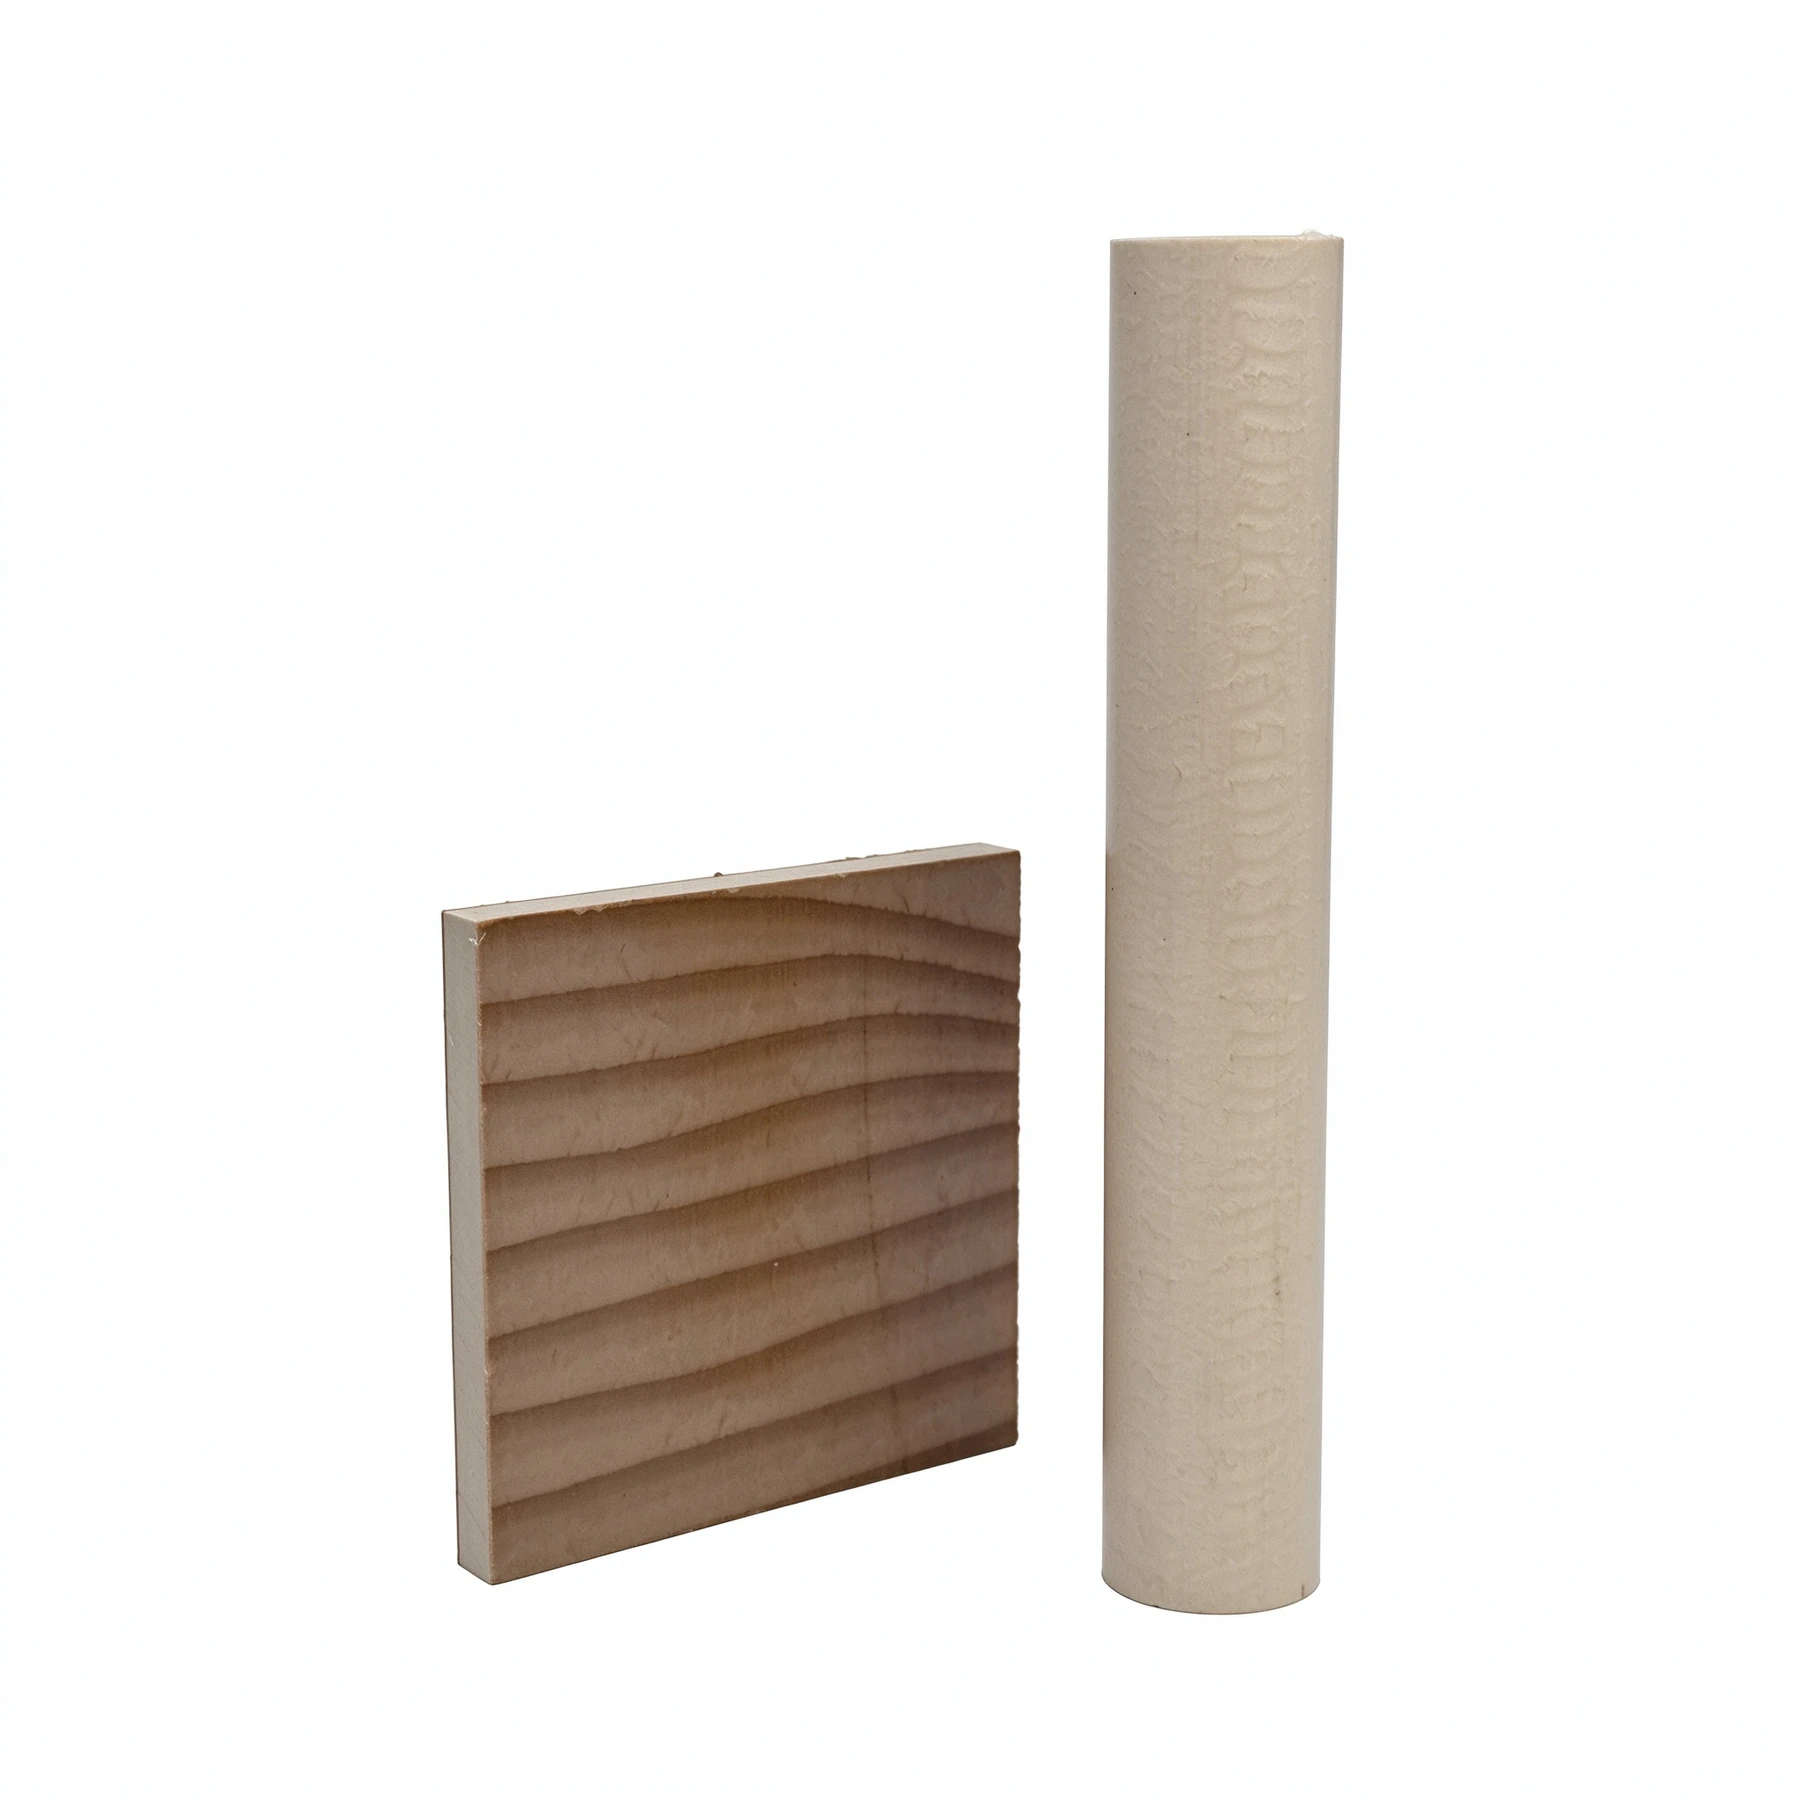
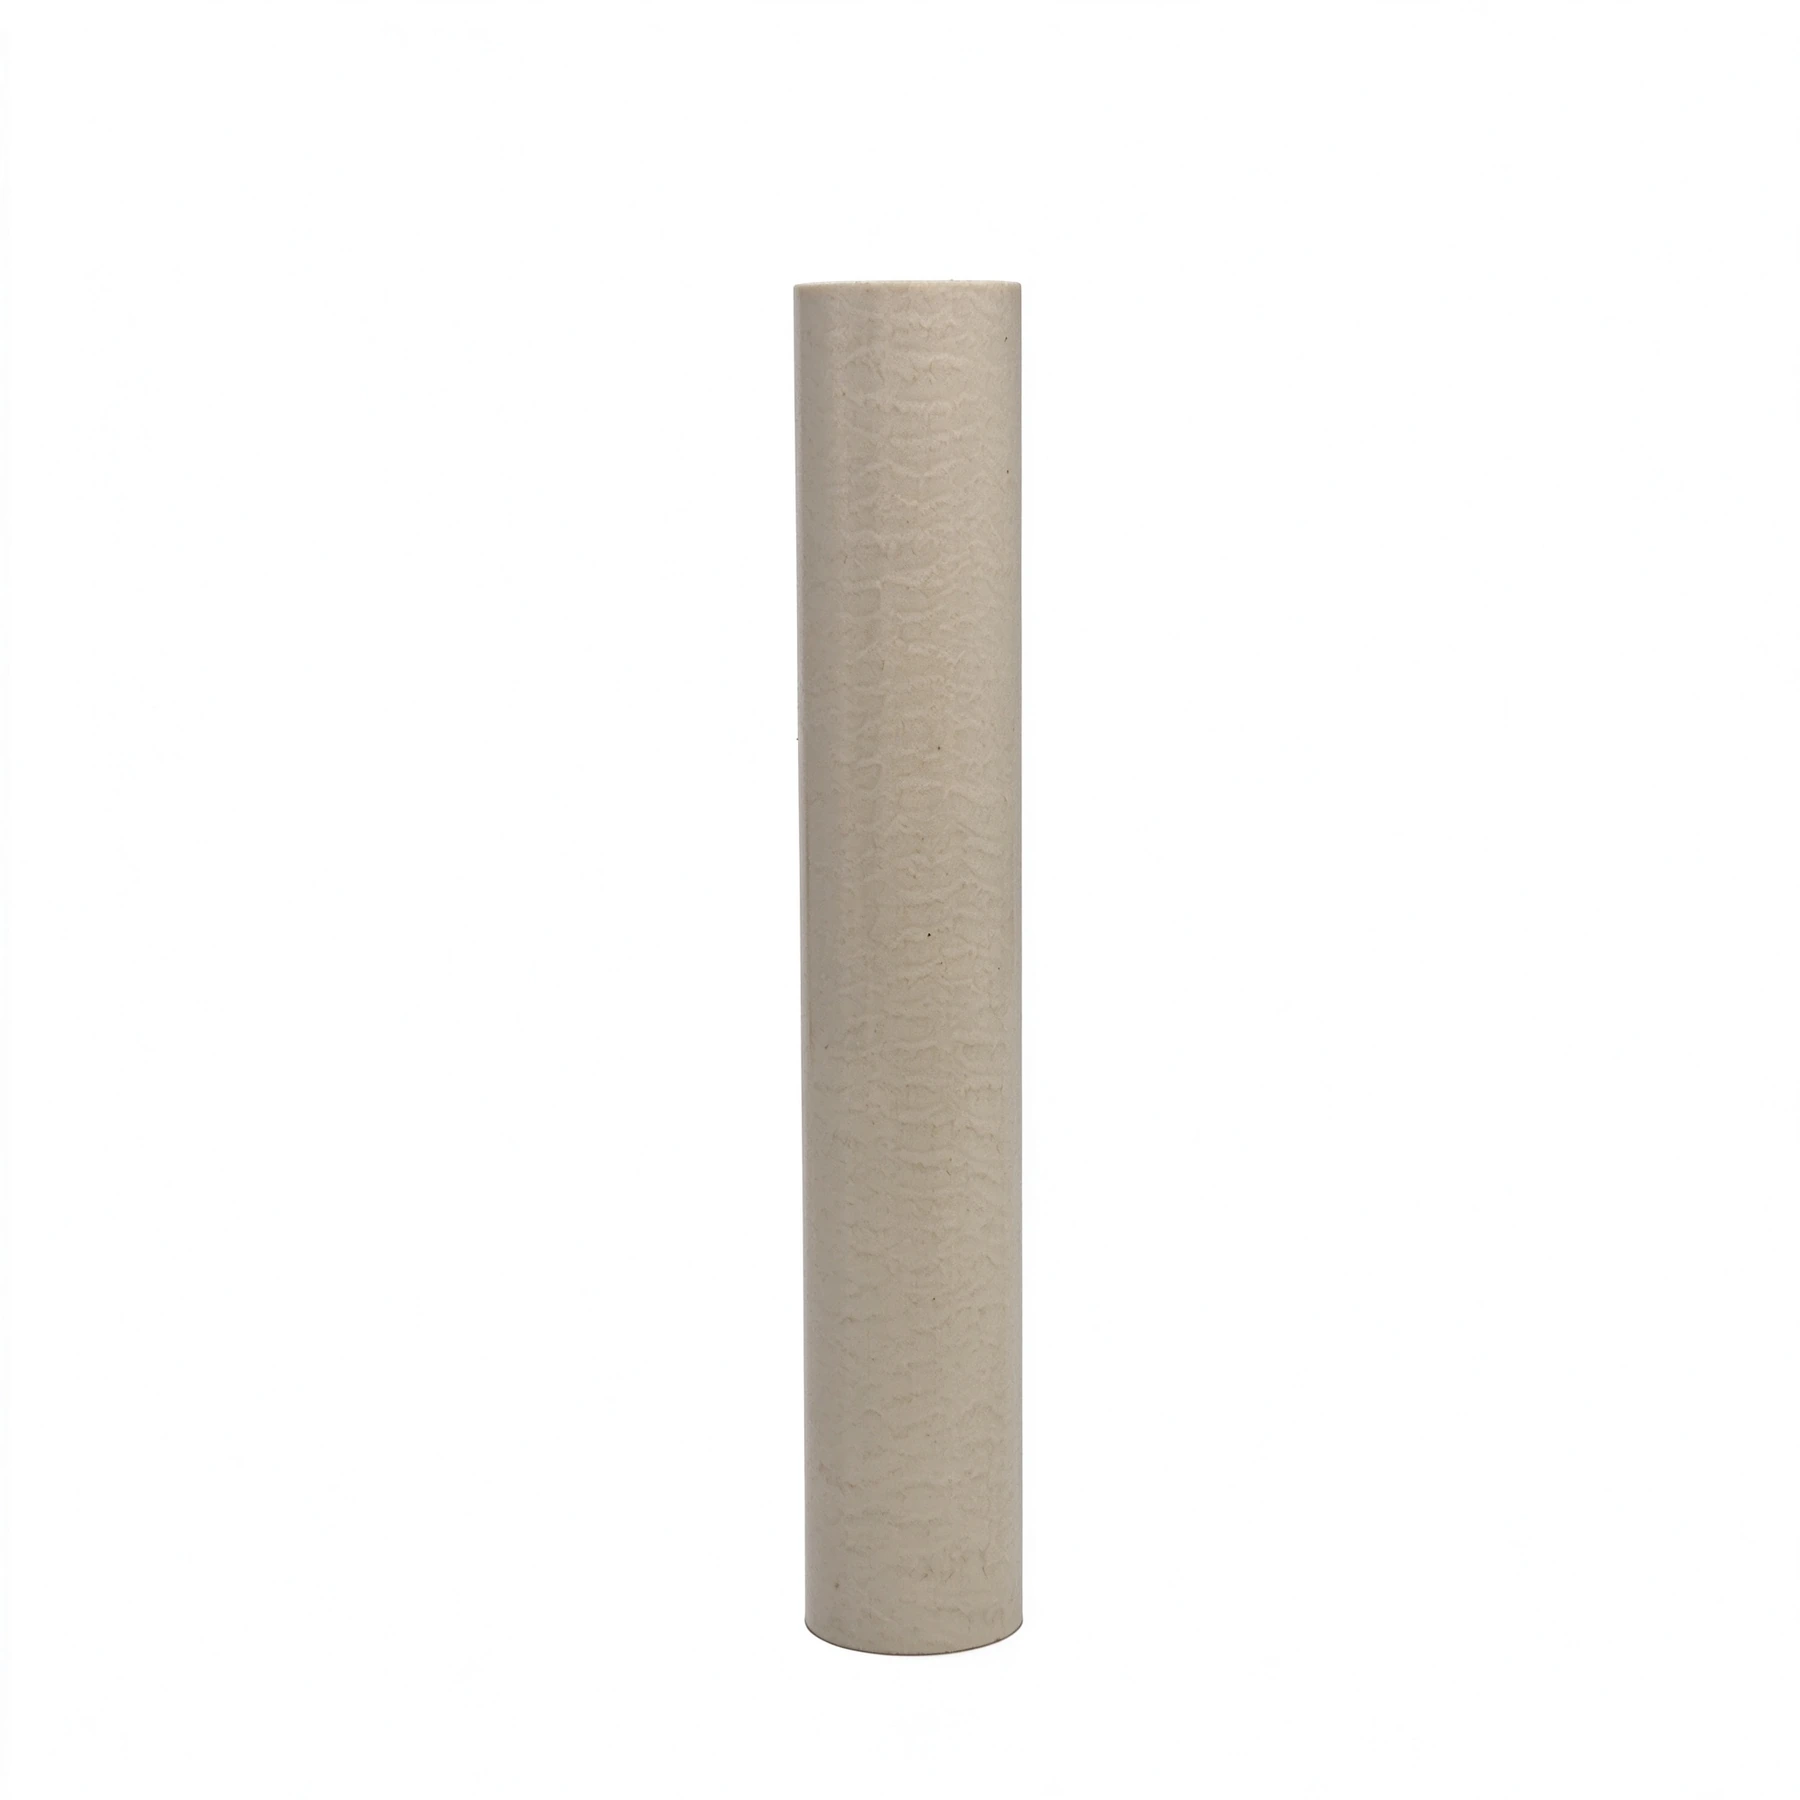
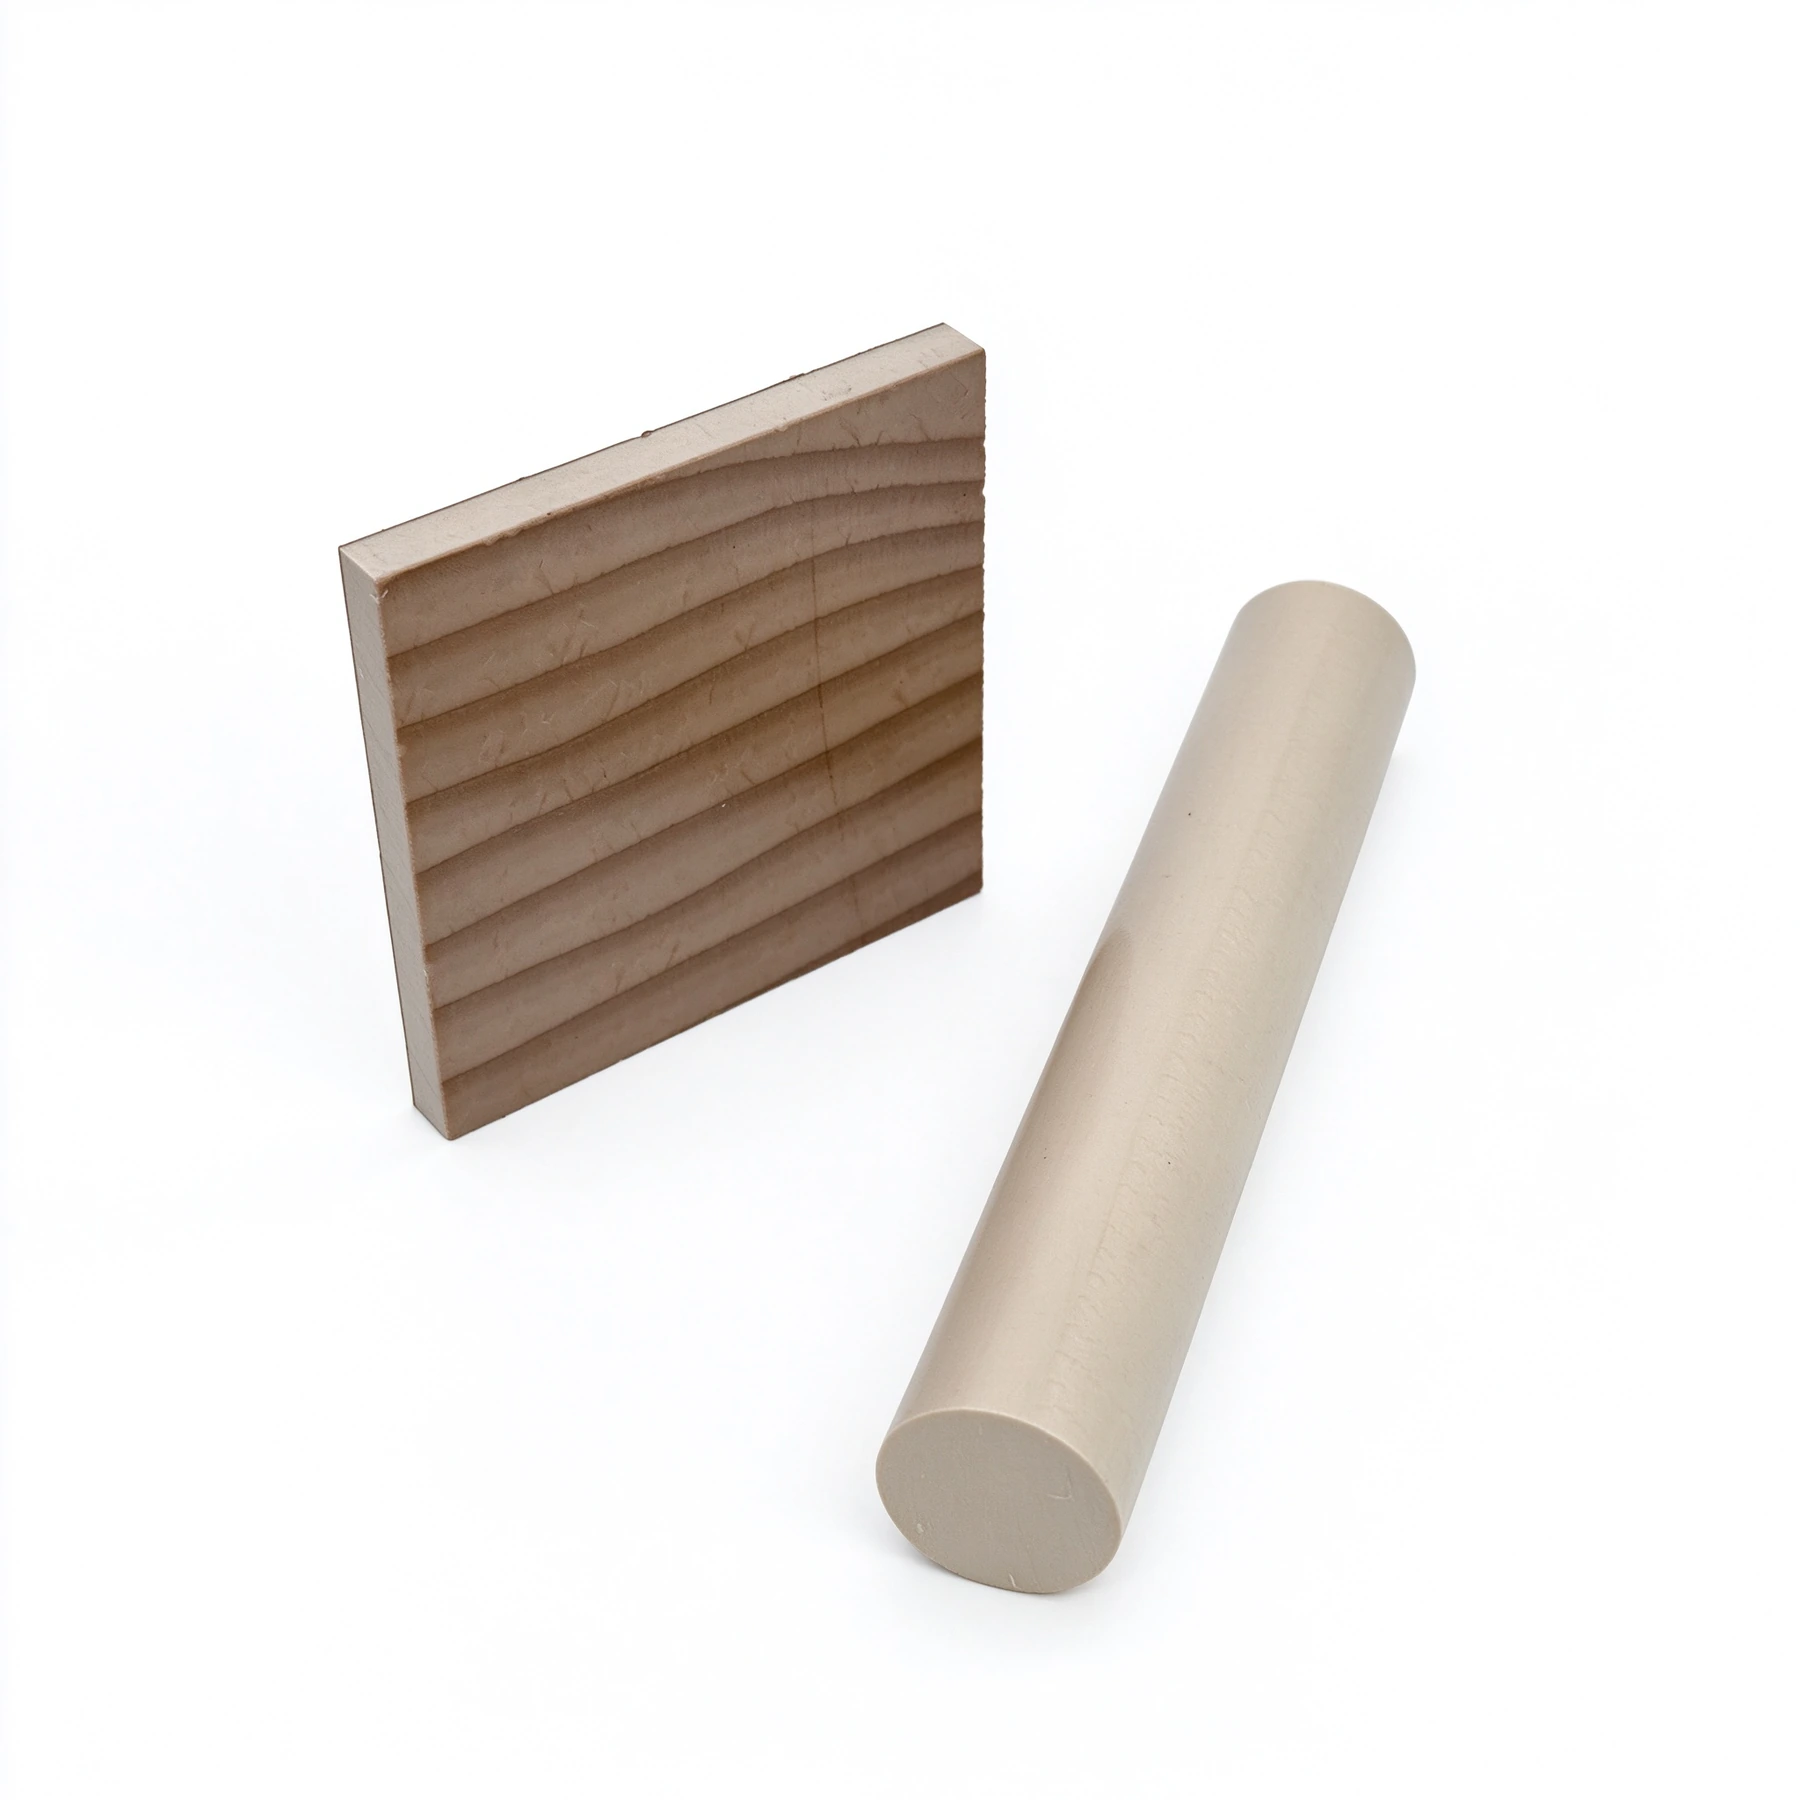
LCP stock — view 01
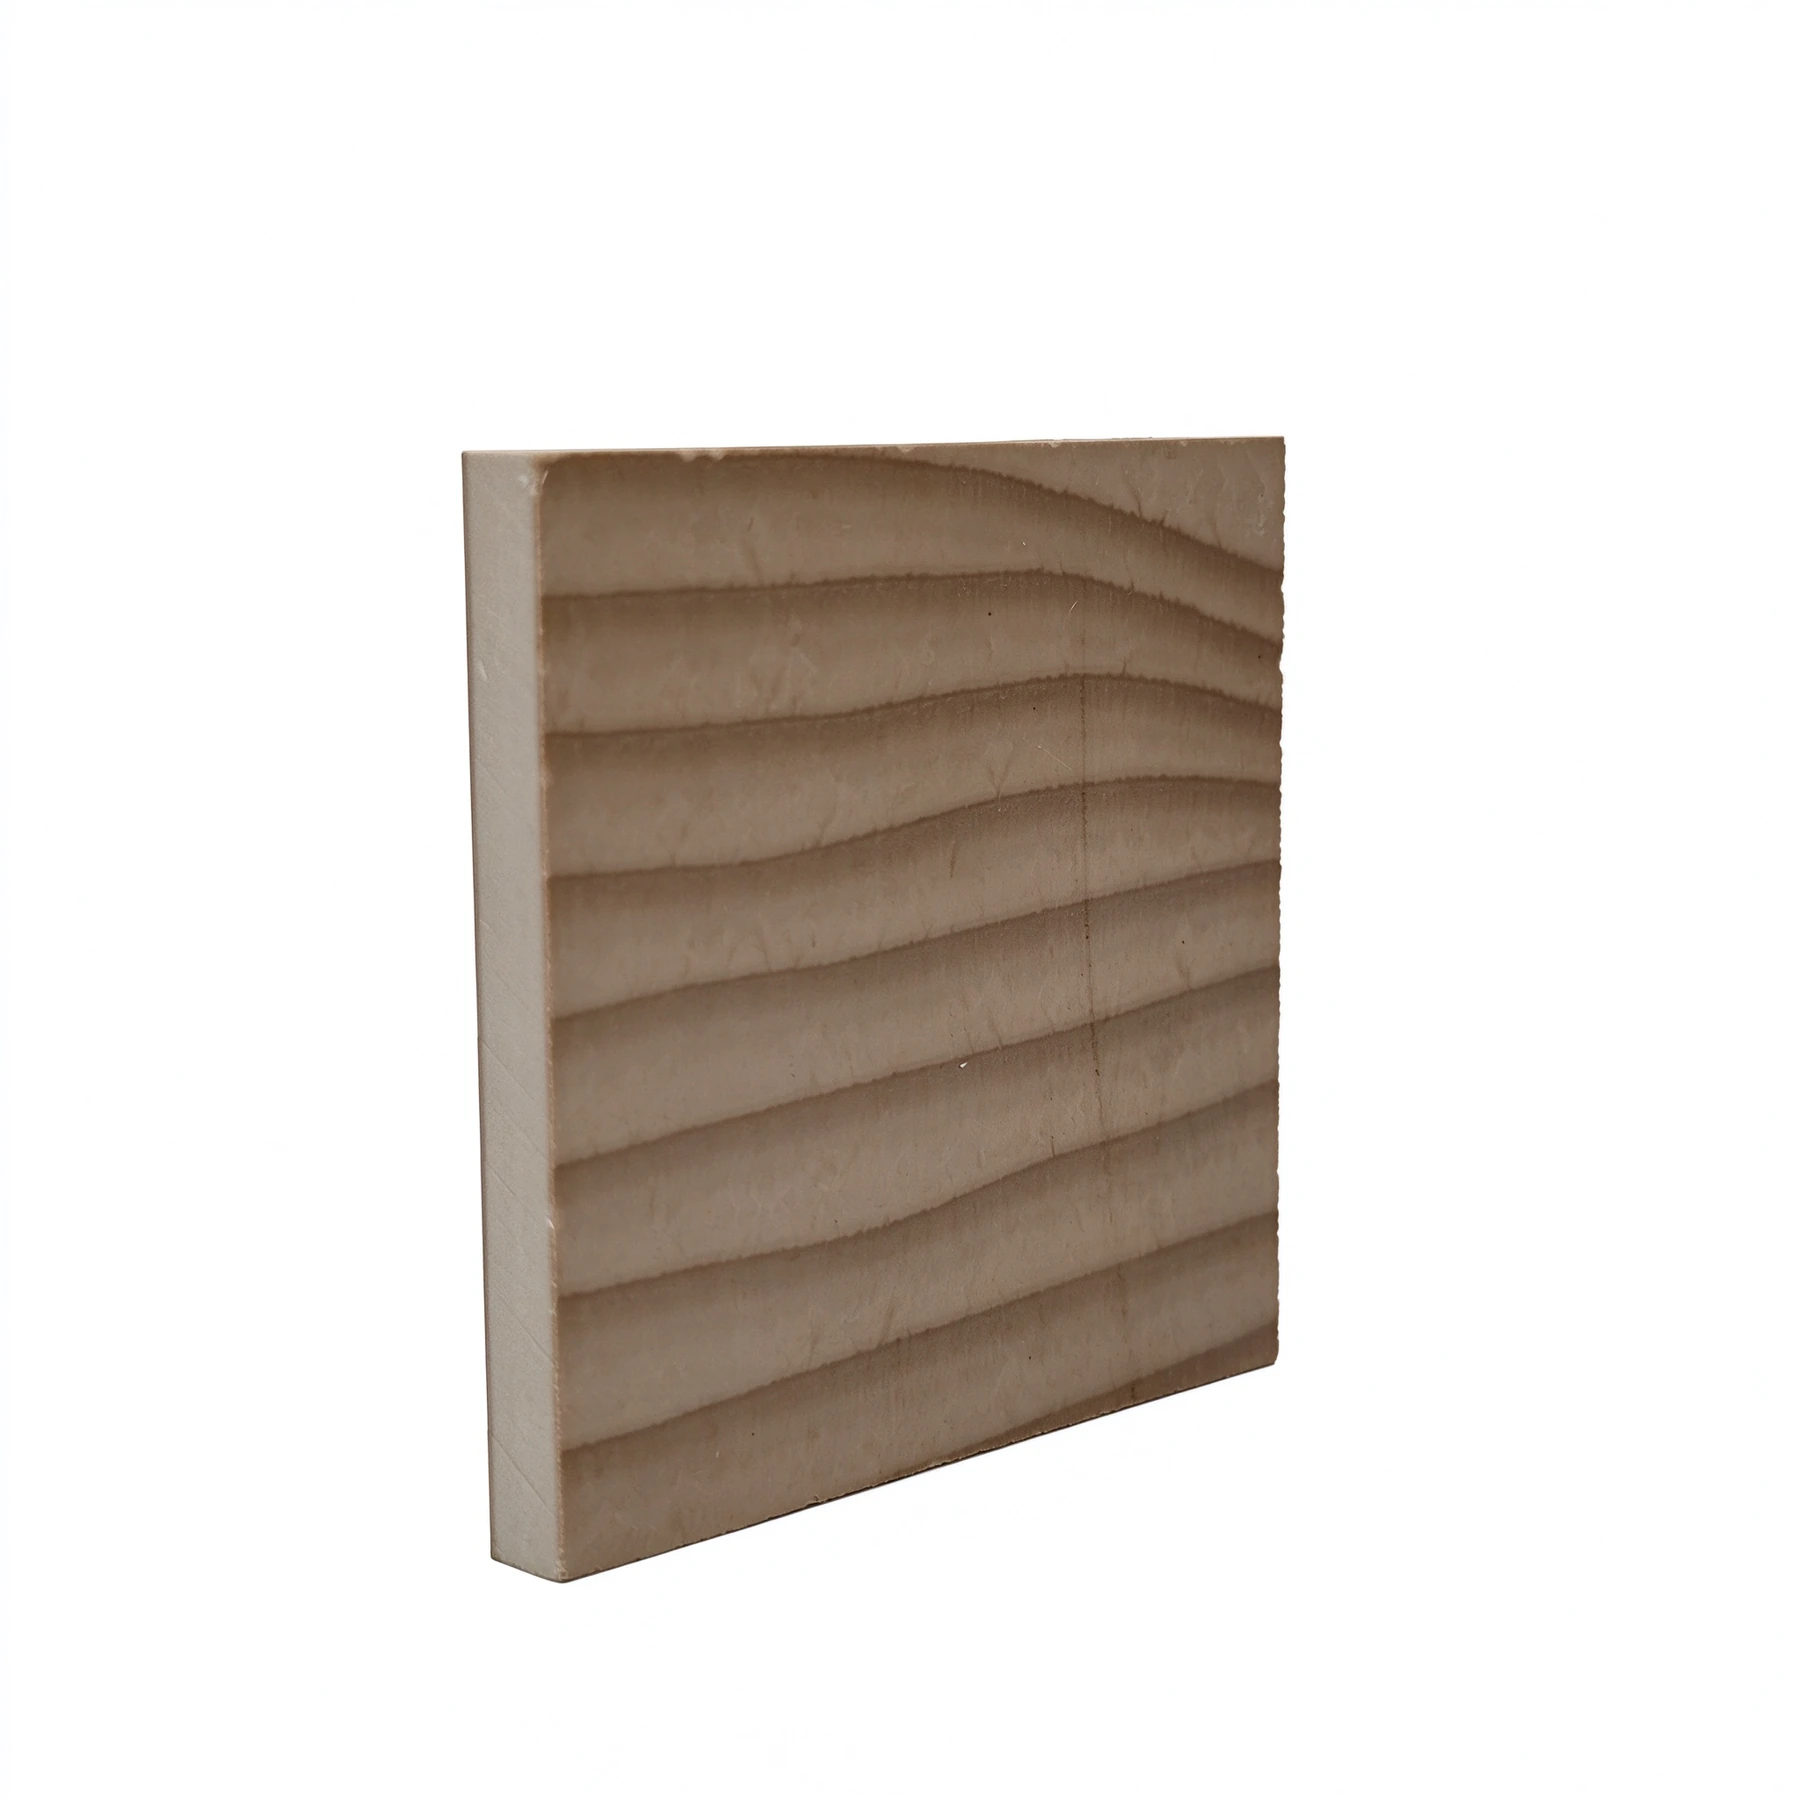
Liquid crystal polymer flows into very thin molded sections and is used for precise, heat-resistant electronic components.




For a small molded LCP component, show Aria the thin sections, contact locations and critical dimensions on the drawing. We help you discuss the selected grade and manufacturing requirements against the part’s function. Include reinforcement and any required electrical or flame-rating documentation in the same review.
| Property | Details |
|---|---|
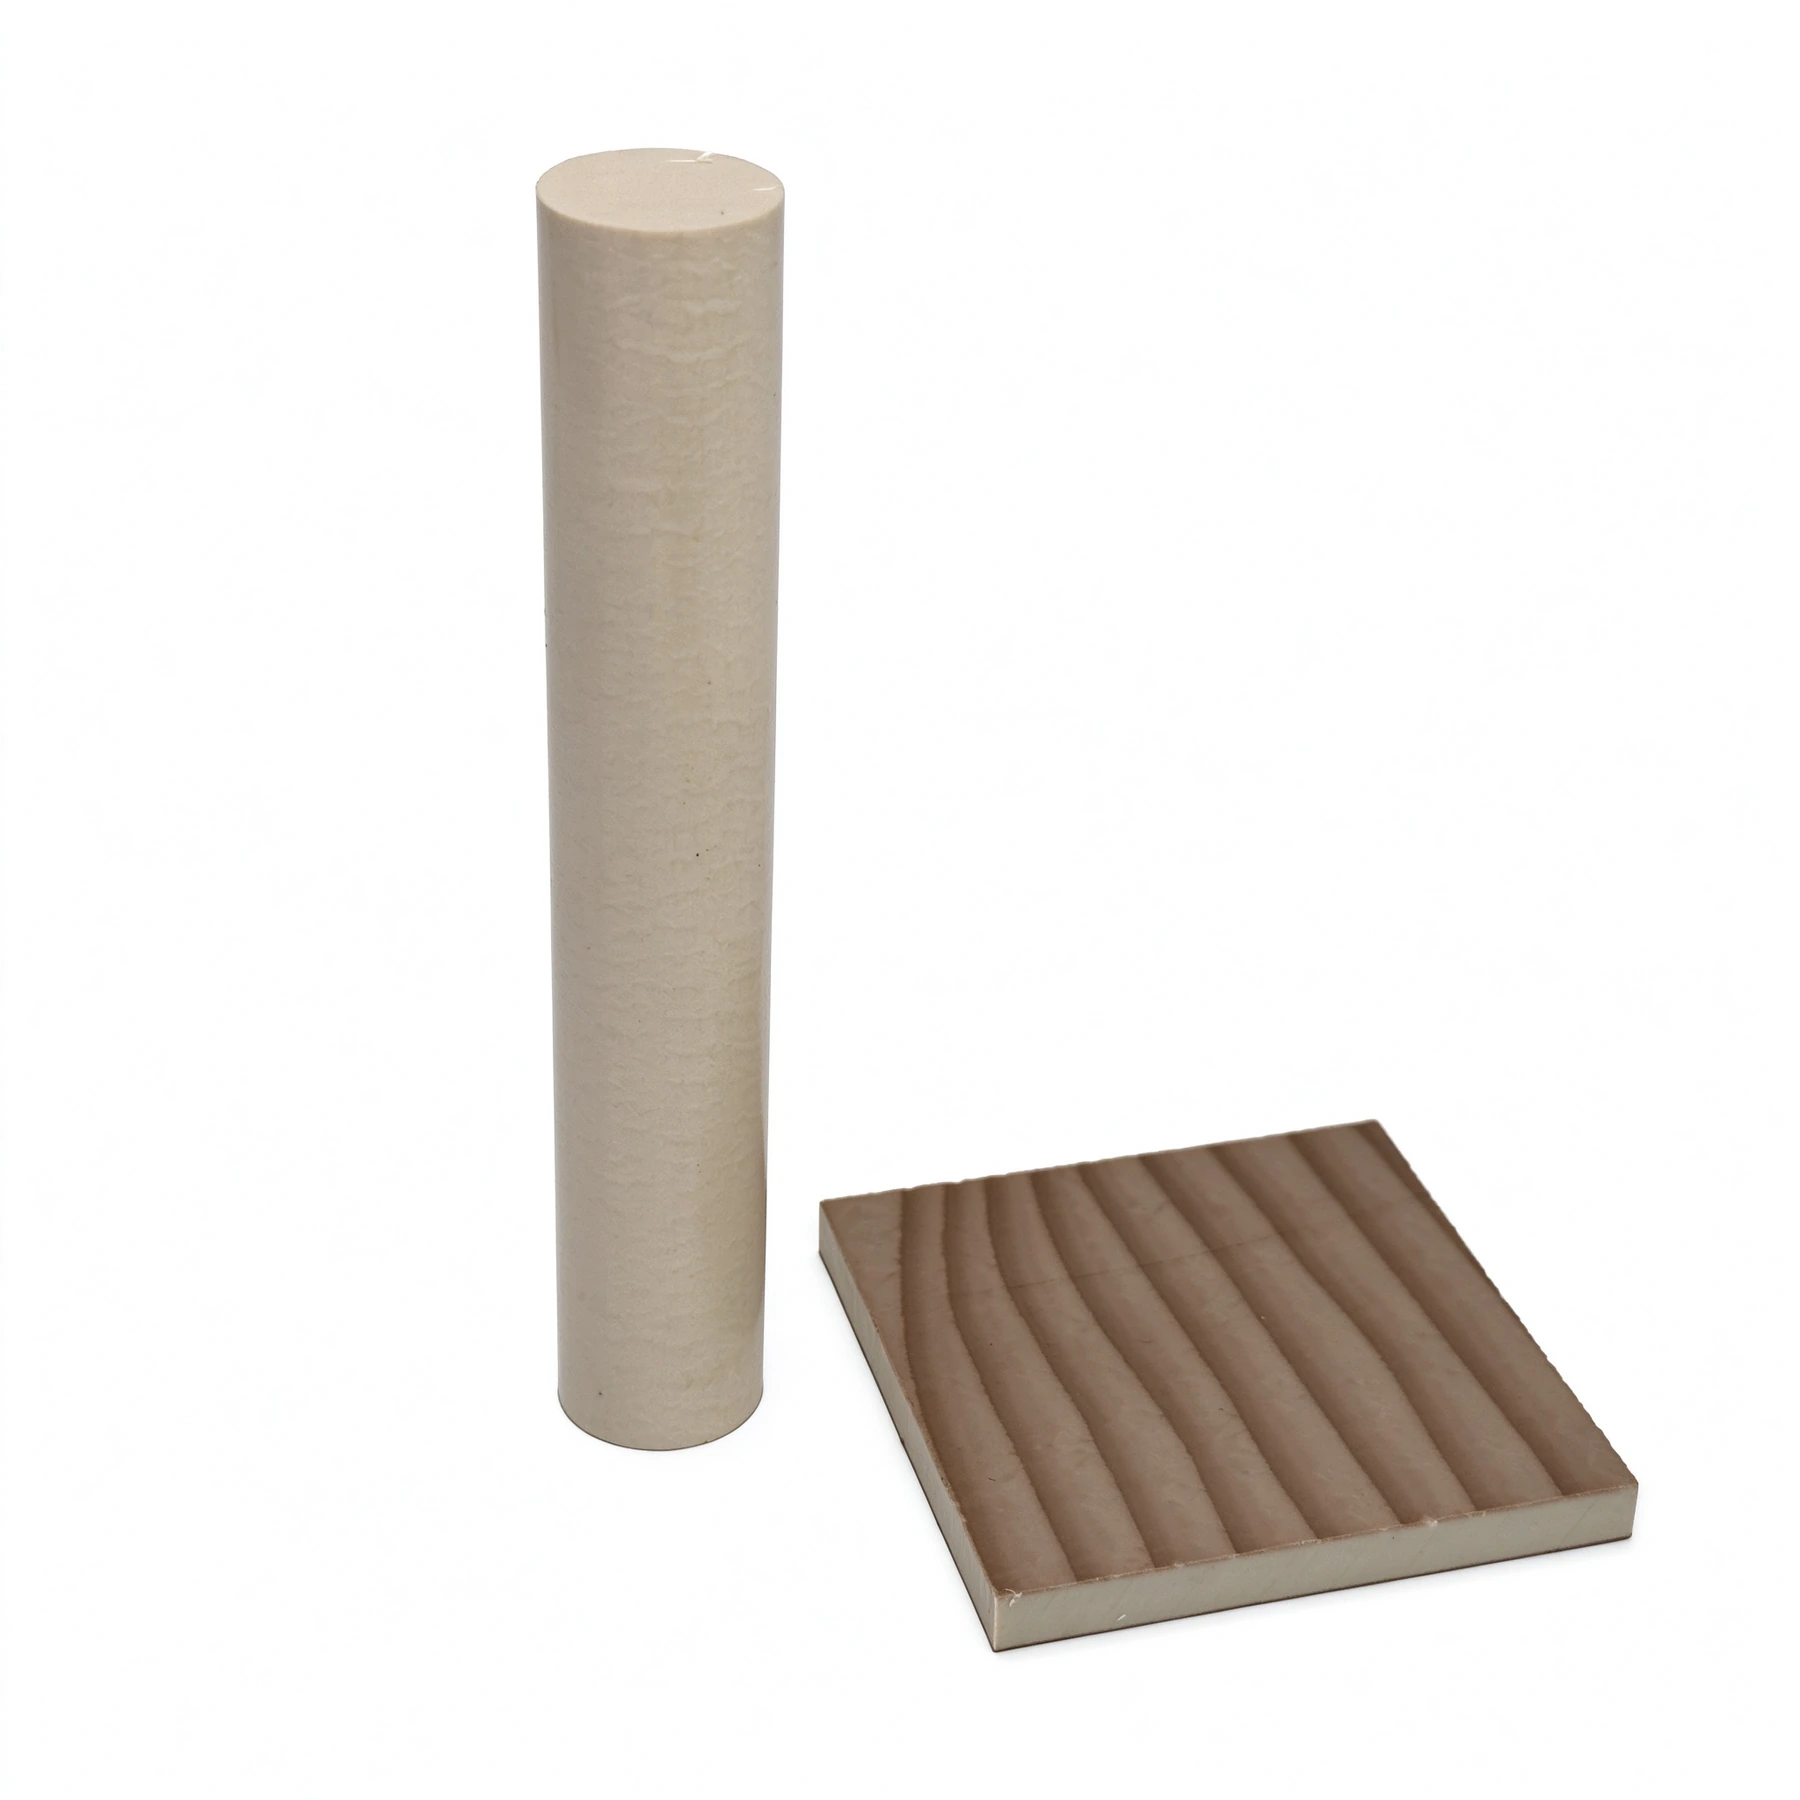
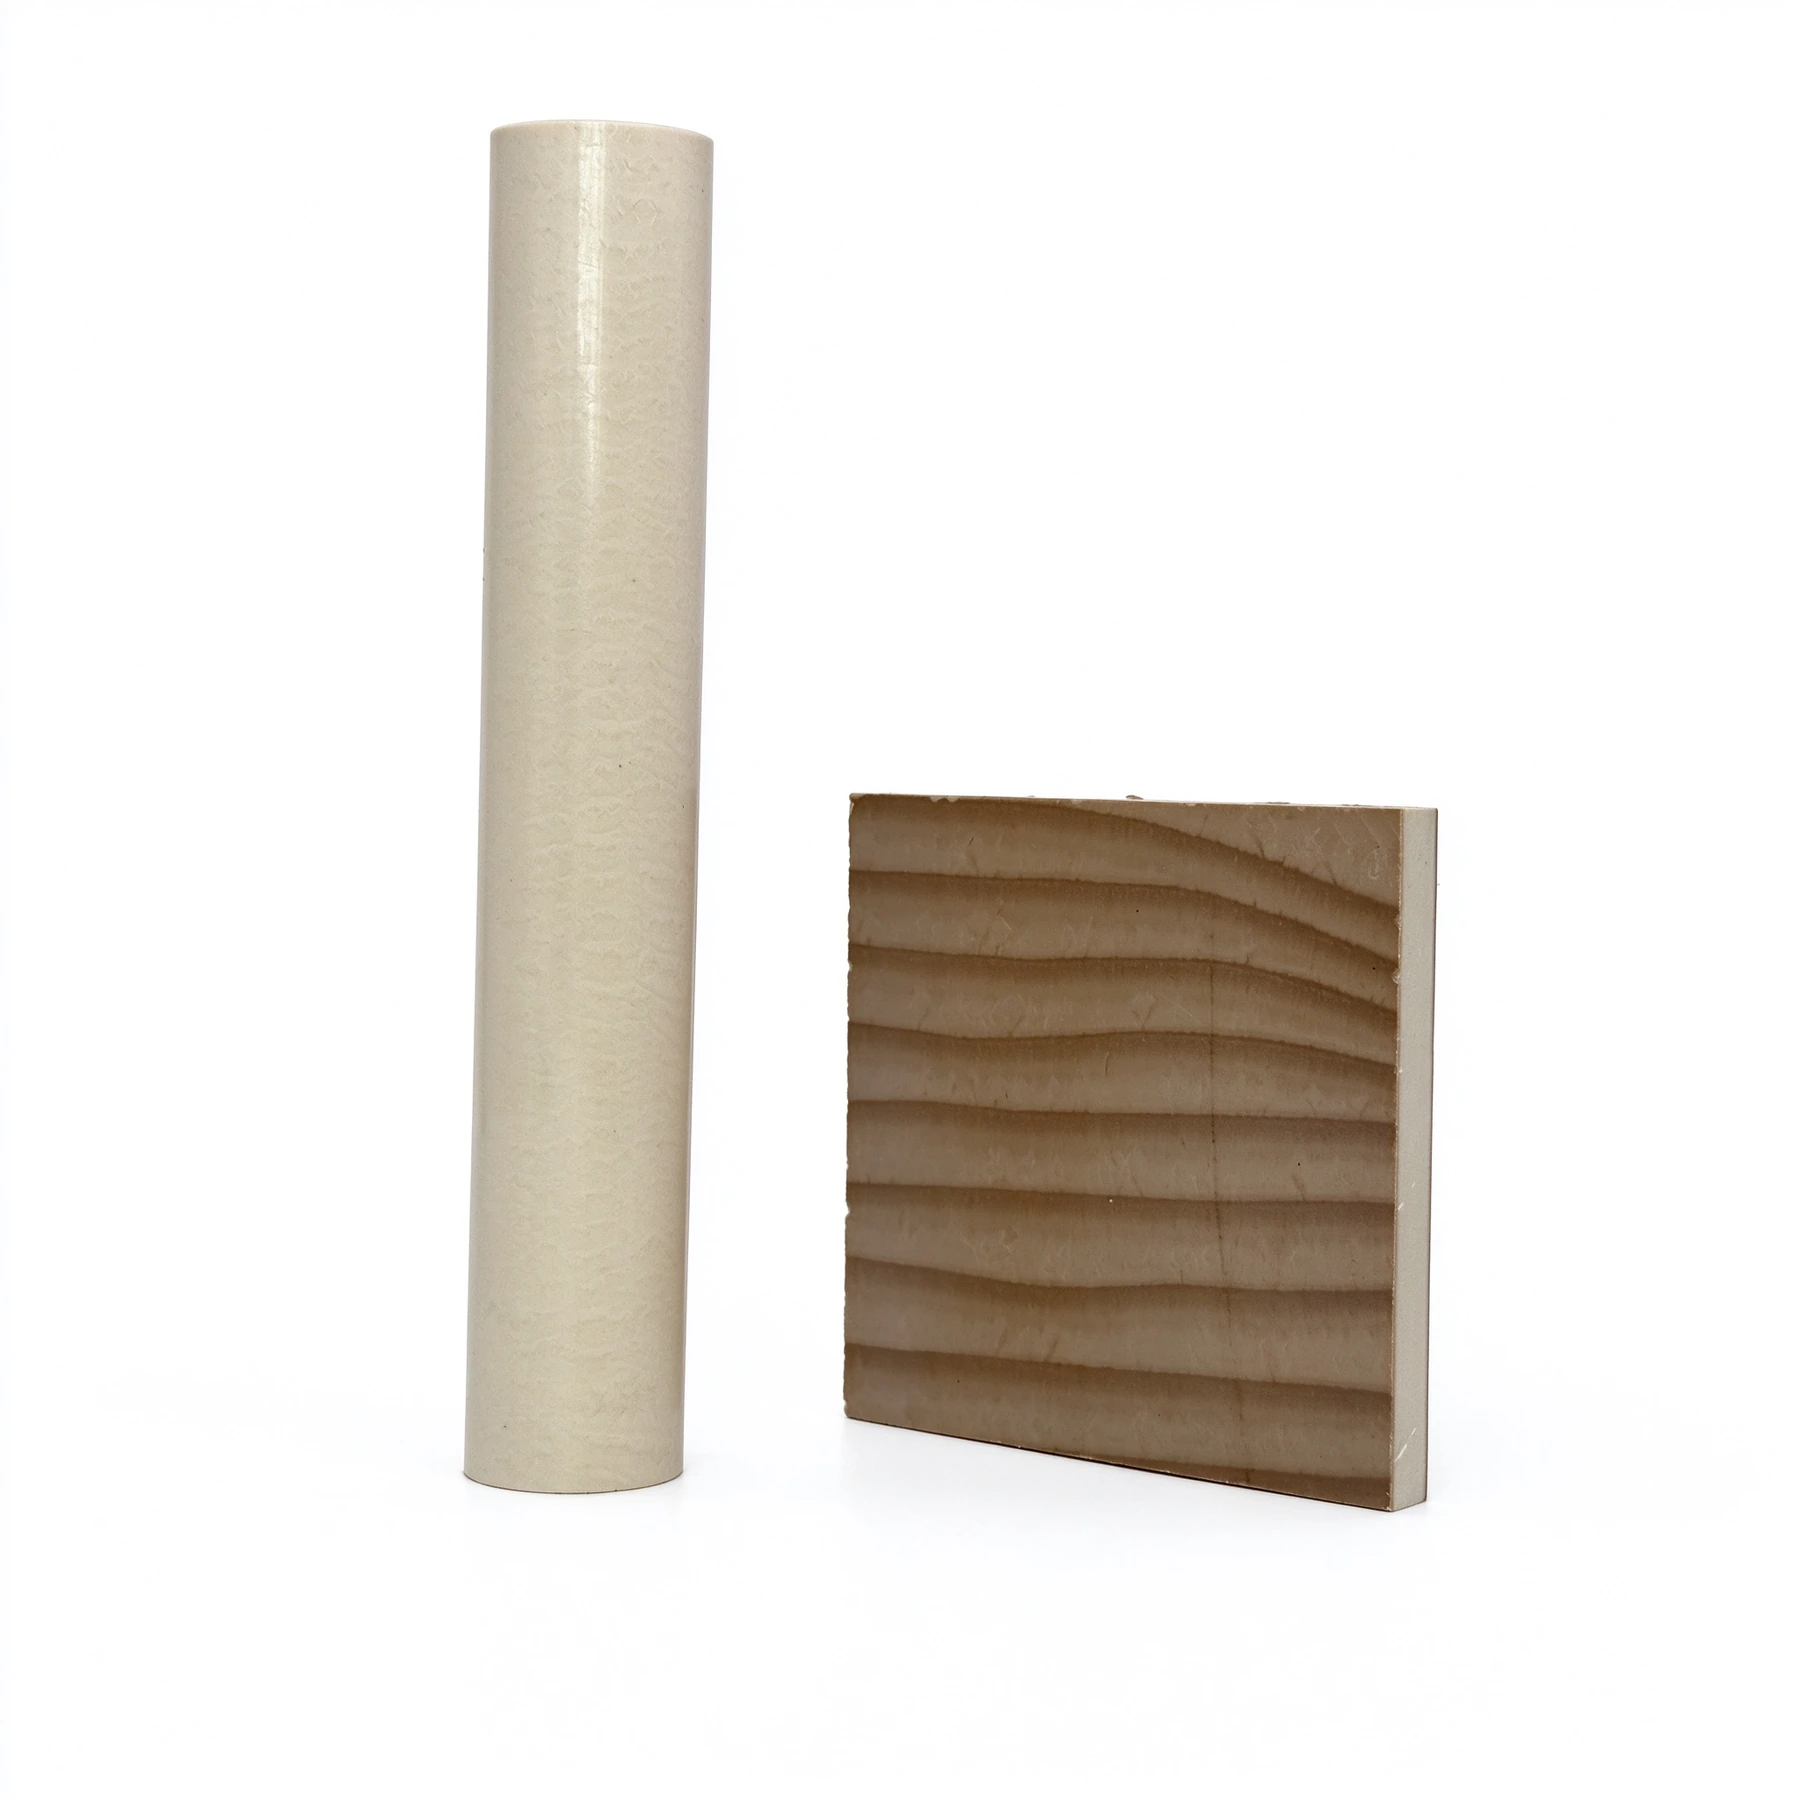
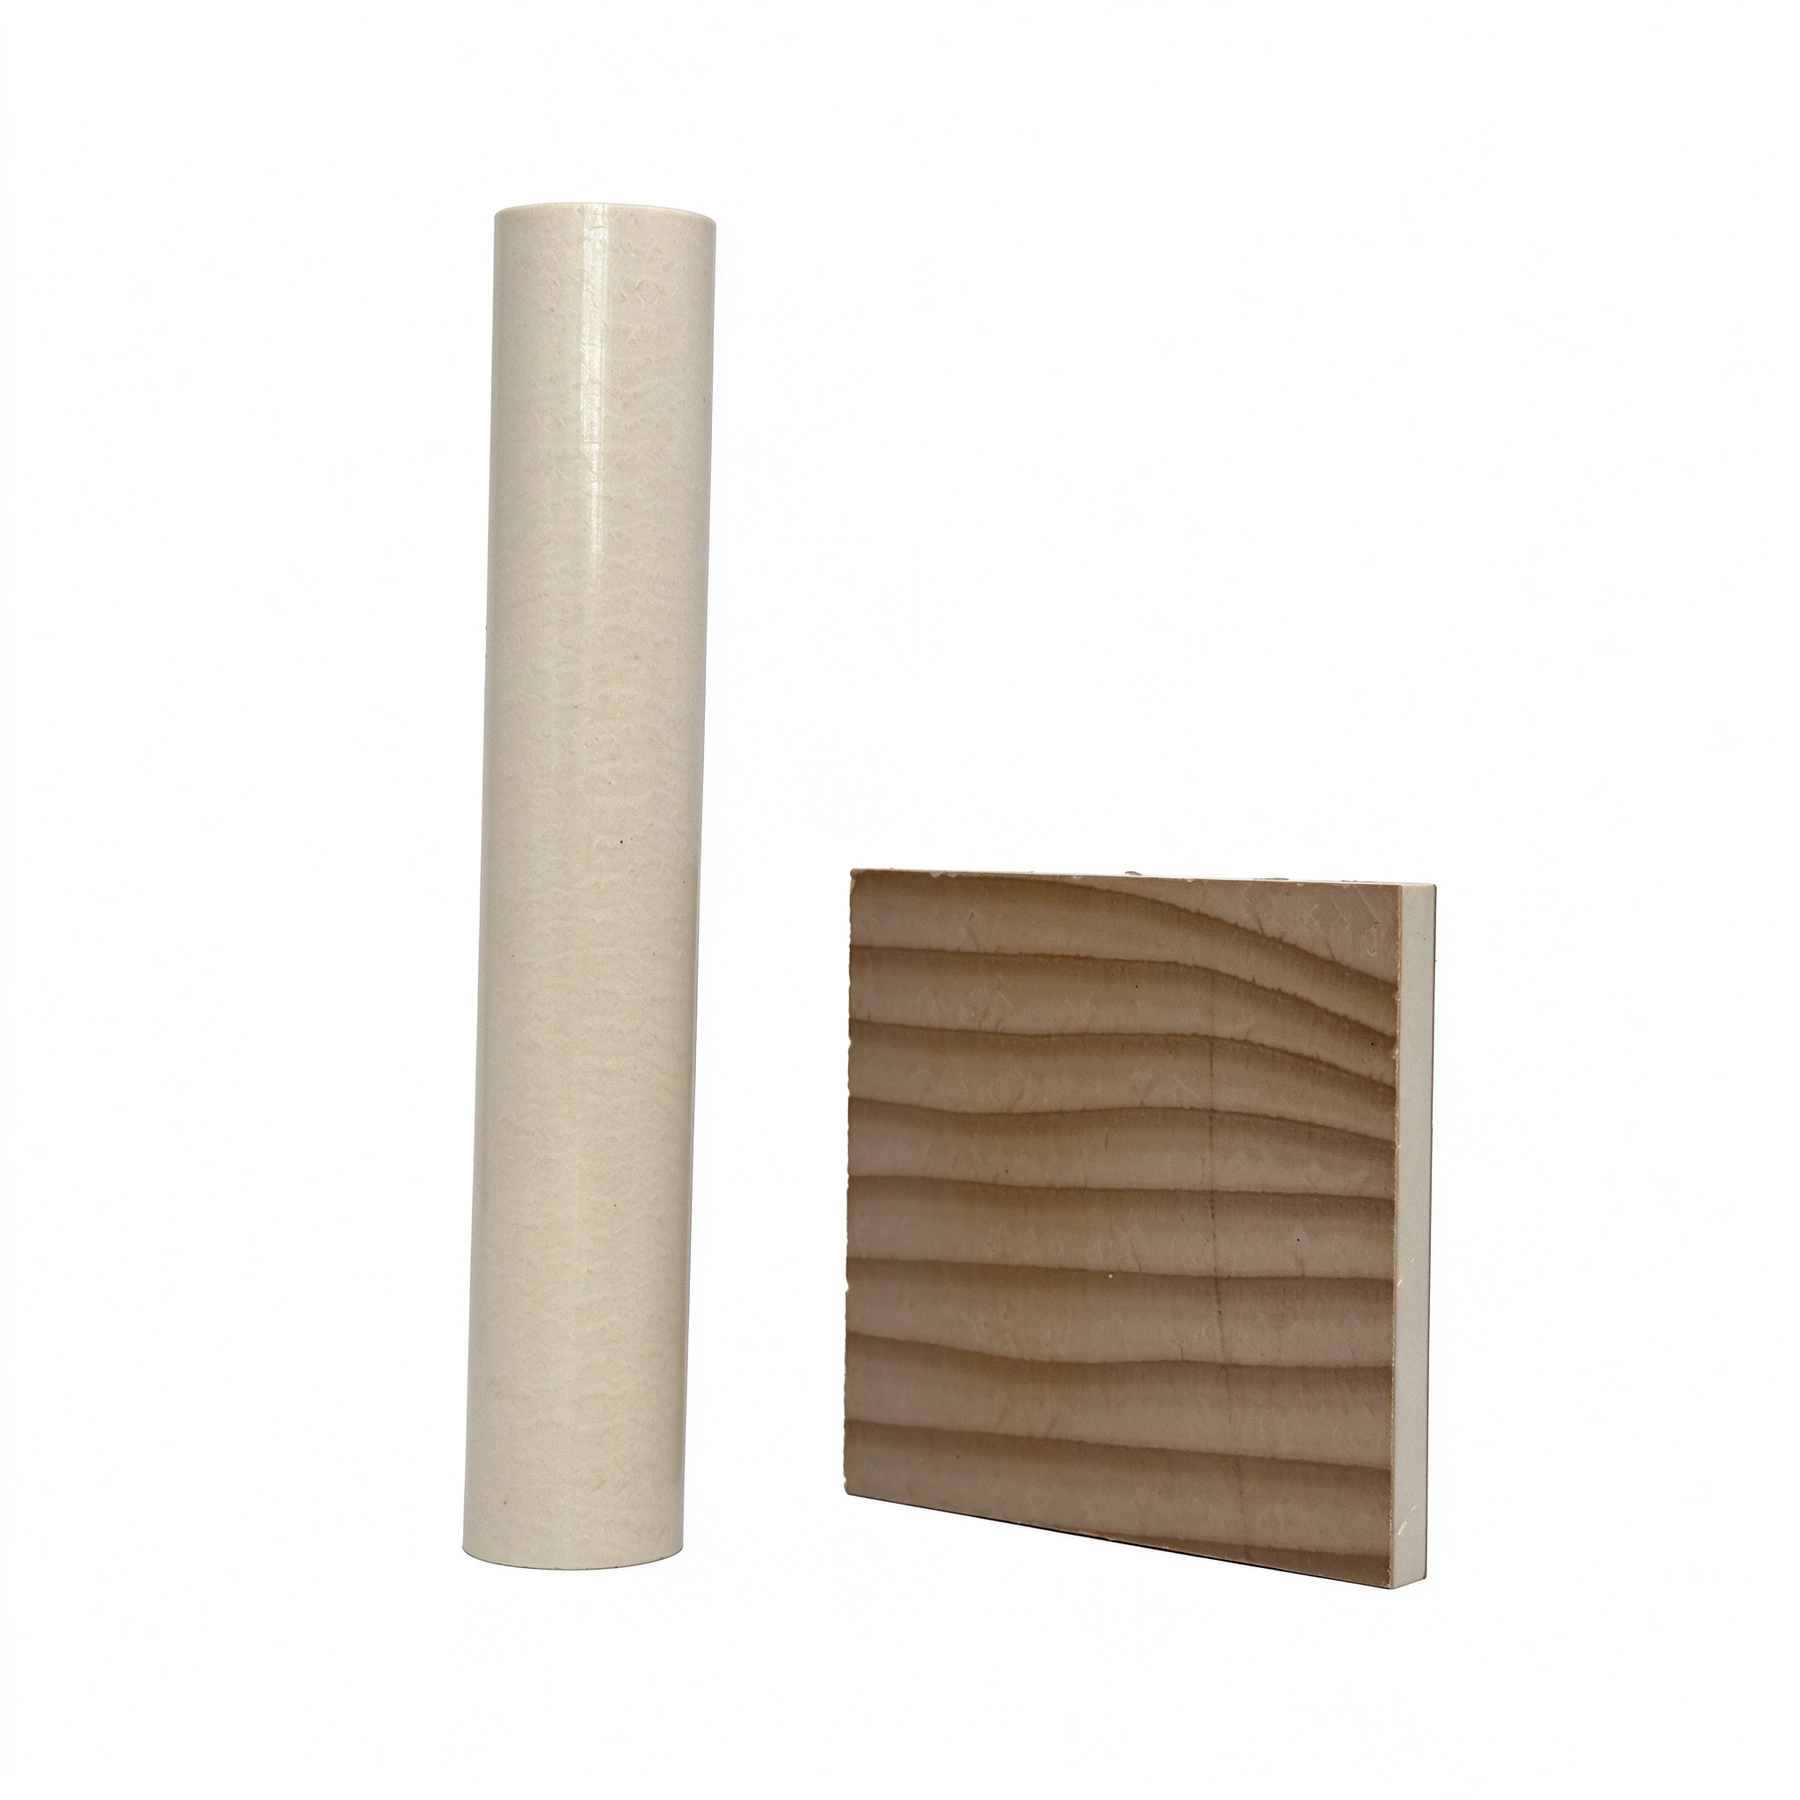
| Colors | Natural tan / beige, Black |
| Special properties | Low expansion and useful dielectric performance; flame rating and glass/mineral reinforcement must be confirmed for the chosen grade. |
Detailed values describe Celanese Vectra A950, unfilled LCP. Family ranges are broader selection references and may include different grades or reinforcement levels. Confirm the selected grade, condition and test method for your part.
| Property | Metric | Imperial | Test method / conditions |
|---|---|---|---|
| Density | 1.40 g/cm³ | 0.0506 lb/in³ | ISO 1183 · 23°C · Reference: Celanese Vectra A950, unfilled LCP |
| Molding Shrinkage (transverse) | 0.7 % | 0.7 % | ISO 294-4 · Flow direction, 0% · Reference: Celanese Vectra A950, unfilled LCP |
| Tensile Modulus | 7,800 MPa | 1,131,000 psi | ISO 527 · 23°C · Reference: Celanese Vectra A950, unfilled LCP |
| Tensile Stress at Break | 148 MPa | 21,500 psi | ISO 527 · 5 mm/min · Reference: Celanese Vectra A950, unfilled LCP |
| Tensile Strain at Break | 5.7 % | 5.7 % | ISO 527 · 5 mm/min · Reference: Celanese Vectra A950, unfilled LCP |
| Flexural Modulus | 9,100 MPa | 1,320,000 psi | ISO 178 · 23°C · Reference: Celanese Vectra A950, unfilled LCP |
| Flexural Strength | 160 MPa | 23,200 psi | ISO 178 · 23°C · Reference: Celanese Vectra A950, unfilled LCP |
| Charpy notched impact (23°C) | 95 kJ/m² | 45 ft·lb/in² | ISO 179/1eA · 23°C · Reference: Celanese Vectra A950, unfilled LCP |
| Melting Temperature | 280 °C | 536 °F | ISO 11357 · 10°C/min · Reference: Celanese Vectra A950, unfilled LCP |
| HDT (1.80 MPa) | 193 °C | 379 °F | ISO 75-1/-2 · 1.80 MPa · Reference: Celanese Vectra A950, unfilled LCP |
| Vicat softening temperature | 145 °C | 293 °F | ISO 306 · 50N, 50°C/h · Reference: Celanese Vectra A950, unfilled LCP |
| Water Absorption | 0.06 % | 0.06 % | Sim. ISO 62 · 2mm · Reference: Celanese Vectra A950, unfilled LCP |
| Oxygen Index | 35 % | 35 % | ISO 4589 · Reference: Celanese Vectra A950, unfilled LCP |
| Flammability | V-0 (UL94) | V-0 (UL94) | IEC 60695-11-10 · 0.42 mm · Reference: Celanese Vectra A950, unfilled LCP |
| Property | Family reference |
|---|---|
| Material class | High-performance plastic |
| Density (g/cm³) | 1.35–1.70 |
| Tensile strength (MPa) | 110–185 |
| Elongation at break (%) | 1–7 |
| Elastic modulus (GPa) | 8–25 |
| Hardness | R80–R90 |
| Temperature reference (°C) | HDT 180–280 |
Thin-wall and precision injection molding. The supplied drying reference is 150°C for four hours; follow the selected grade datasheet. Gate position and flow direction are critical. Keep weld lines away from loaded areas and confirm reinforcement, drying and flame-rating requirements.
Excellent melt flow, low molding shrinkage and thermal expansion, low moisture uptake and useful dielectric behavior. Some designs use walls below 0.3 mm.
Strong flow-direction dependence and weak weld lines constrain mechanical design. Unfilled grades can be brittle; colors and appearance finishing are limited.
Compare materials for the loads, temperature and environment your part will face.
We review tool access, geometry and material choice before manufacturing.
Dimensional checks and inspection reports for the critical features on your drawing.
Gate position and flow direction are critical. Keep weld lines away from loaded areas and confirm reinforcement, drying and flame-rating requirements. Laser marking; circuit metallization is possible with suitable MID/LDS material and process selection. Decorative painting is less common.
Precision connectors, surface-mount components, high-frequency antenna parts, optical modules and thin-wall electronics.
Thin-wall and precision injection molding. The supplied drying reference is 150°C for four hours; follow the selected grade datasheet.
Laser marking; circuit metallization is possible with suitable MID/LDS material and process selection. Decorative painting is less common.
Gate position and flow direction are critical. Keep weld lines away from loaded areas and confirm reinforcement, drying and flame-rating requirements.
Natural tan or beige. Black; custom colors are limited.
Upload your CAD files and tell us the material and quantity you need.
Talk to an engineer